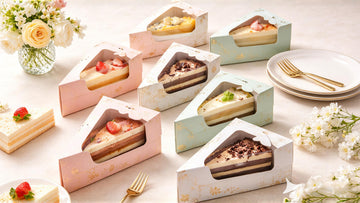

When bakery brands switch to more sustainable packaging, one of the most common mistakes is choosing paper that looks recyclable. Kraft paper bags, white paperboard boxes, and pastry boxes with transparent windows all carry a natural, eco-friendly appearance. But once they reach a recycling facility, their appearance means very little.
What actually determines whether packaging can be recycled is how easily its paper fibers can be separated, whether coatings interfere with screening equipment, and whether food residue exceeds acceptable contamination levels.
The central challenge of recyclable bakery packaging is a familiar one: food protection requires effective barriers, while recycling works best with simple, easily separable materials. Finding the right balance between these two requirements is where better packaging design begins.

The recyclability of paper-based packaging largely depends on whether its fibers can be effectively separated during the pulping process. Uncoated paperboard and corrugated cardboard generally break down easily in standard hydrapulpers, allowing their fibers to be recovered with relatively high efficiency and consistent recycling value.
However, bakery packaging is rarely made from paper alone. Grease resistance requires protective coatings, product visibility calls for transparent windows, and premium branding often involves lamination or specialty printing. When these additional materials bond too tightly with the paper fibers, recycling facilities face two major challenges.
Take polyethylene (PE) or polypropylene (PP) laminated paperboard as an example. These polymers do not dissolve during pulping. Instead, they break into plastic fragments ranging from a few millimeters to several centimeters. These fragments can accumulate on screening equipment, block screens, and increase cleaning and maintenance costs.
Printing can create a less obvious problem. Paperboard covered with extensive UV coatings or certain solvent-based inks can be more difficult to deink. This may reduce the quality of recovered fibers, forcing recycling facilities to downgrade the material or reject it altogether.
In other words, whether a paperboard package is recyclable has little to do with how much it looks like paper. What matters is how many non-paper materials are attached to it and how easily they can be removed during recycling.
The paper materials commonly used in bakery packaging can have very different recycling performance. Understanding their characteristics helps brands make more informed packaging decisions.
1. Kraft Paper
Kraft paper is typically made from unbleached virgin pulp. Its long fibers provide good strength and durability, while its natural brown appearance gives packaging an understated, eco-friendly look.
However, kraft paper has relatively limited printing versatility. Its darker background can affect color accuracy and print vibrancy. To achieve brighter, cleaner designs, brands may need to apply a full layer of white ink before printing, which can increase production costs.
From a recycling perspective, uncoated kraft paper is generally well accepted by paper recycling systems. The main condition is to avoid adding difficult-to-separate materials such as plastic lamination or large amounts of adhesive from labels and stickers.

2. White Paperboard (SBS)
Solid Bleached Sulfate (SBS) paperboard is made from bleached virgin pulp and features a smooth, refined surface. Its excellent printability makes it a popular choice for premium bakery boxes, high-quality product photography, and detailed packaging graphics.
The challenge is that premium SBS packaging often comes with additional finishing processes, including lamination and foil stamping. Plastic-laminated paperboard can be difficult to recycle because the film and paper fibers require specialized separation processes. Many municipal recycling programs do not accept this type of packaging.
For brands prioritizing recyclable paper bakery boxes, unlaminated SBS with carefully selected printing and finishing options is generally a more practical choice.
3. Corrugated Cardboard
Corrugated cardboard has one of the most established recycling systems in the paper packaging industry. Old Corrugated Containers (OCC) are among the most widely collected and recycled paper grades worldwide.
However, bakery applications rarely use completely untreated corrugated board. Grease-resistant coatings and food contamination are the main variables affecting its recyclability.
There is some encouraging evidence: research on pizza boxes has shown that ordinary grease contamination, typically around 1–2% by weight, does not necessarily prevent corrugated cardboard from being recycled.
However, heavily saturated bakery boxes may still be classified as contaminated paper waste, depending on local recycling standards and facility capabilities.
4. Recycled Paperboard
Recycled paperboard generally comes in two common forms: uncoated recycled board, which often has a gray appearance and visible fiber variations, and coated recycled paperboard, commonly known as Clay Coated News Back (CCNB), which features a white printable surface and a gray recycled-paper backing.
CCNB offers a printing appearance closer to virgin white paperboard at a lower material cost, making it a practical option for mass-produced bakery boxes.
Its main limitation lies in its recycled fibers. These fibers are generally shorter and weaker than virgin fibers, which can make the board more prone to cracking along tight folds. Repeated recycling also gradually reduces fiber strength.
As a result, recycled paperboard may not be suitable for every packaging structure, particularly boxes that require substantial stacking strength or load-bearing performance.
Grease resistance is essential for many bakery packaging applications. Traditional solutions include PE lamination and fluorinated grease-resistant treatments. However, both come with environmental concerns. PE films can interfere with paper recycling, while certain fluorinated substances face increasing regulatory scrutiny due to concerns surrounding PFAS.
Alternative solutions include water-based coatings and mineral-based barrier coatings. Water-based acrylic coatings, for example, can offer better compatibility with standard paper recycling processes when properly formulated. However, their grease resistance may be limited, making them more suitable for short-shelf-life products with relatively low oil content.
For products with high fat content or longer shelf-life requirements, brands may need to accept a trade-off between barrier performance and recyclability. No universal coating solution works equally well for every bakery product.
Transparent windows present another challenge. Some municipal recycling programs accept paper boxes with small plastic windows, provided the windows are limited in size and securely attached. Others require consumers to remove the window or do not accept these packages at all.
For bakery brands that want to maintain product visibility, choosing between PLA and thin PET does not automatically solve the recycling problem. Neither material is typically separated from paperboard by conventional paper recycling systems.
A more practical approach is to reduce the window size or consider die-cut openings combined with a minimal inner film, where suitable. This helps reduce the proportion of non-fiber materials in the overall package.
Lamination is one of the most challenging finishing processes for paper recyclability. Matte lamination certainly adds a premium feel and improves the tactile experience, but plastic films can make paperboard much harder to recycle. Many standard paper recycling systems are not equipped to process these composite structures.
If a premium matte finish is important to the brand, alternatives such as water-based tactile coatings or spot UV finishing are worth considering. Although the visual and tactile effects may differ slightly, these options can help preserve the recyclability of the paperboard, depending on the coating formulation and local recycling requirements.

Developing genuinely recyclable bakery packaging is not about finding one perfect material. It is about minimizing compromises between product protection, visual presentation, production costs, and end-of-life disposal.
Start with simpler packaging structures.
Reducing the number of different materials is one of the most effective ways to improve recyclability. A paperboard box with a paper insert is generally easier to recycle than a combination of paperboard, a plastic window, and a PET tray.
If an inner support is necessary, consider unbleached kraft paper or molded recycled pulp. When the materials are compatible with the local recycling system, they can help simplify disposal without requiring consumers to separate multiple components.
Choose printing methods carefully.
Controlling ink coverage is another important consideration. Large areas of solid, dark printing can increase the deinking burden and potentially reduce the value of recovered paper fibers.
Light-colored backgrounds, selective spot colors, and unprinted areas can create a clean, distinctive visual identity while reducing unnecessary ink coverage. Minimalist packaging design can therefore support both brand presentation and more recycling-friendly material choices.
Match coating performance to the actual product.
Different bakery products have very different grease-resistance requirements. A butter croissant and a heavily frosted, oil-rich cake do not need the same level of barrier protection.
There is little reason to use heavy plastic lamination on products that only require basic grease resistance. For short-shelf-life, low-fat bakery products, a suitable water-based coating may be sufficient.
For products with higher oil content, stronger barrier materials may still be necessary. In these cases, packaging instructions should clearly explain how to separate the paperboard from any non-paper components before disposal, where separation is possible.
Make recycling instructions clear and realistic.
Finally, recyclability should not be treated as a marketing label that can simply be printed on a box. Recycling infrastructure and acceptance standards vary considerably between regions.
What brands can do is reduce material complexity and contamination as much as possible, choose components that are compatible with common recycling systems, and provide clear disposal instructions.
A box labeled "recyclable" but covered in plastic lamination may create more recycling difficulties than a simple, uncoated kraft paper bag that can enter the local paper recycling stream.
If you are planning your next bakery packaging collection, choosing the right paperboard and coating combination is an important first step. The SNFOOD customization team can help you evaluate packaging options based on your product's fat content, shelf-life requirements, and brand positioning.
Contact SNFOOD for customized bakery packaging solutions, wholesale quotations, and practical advice on packaging materials and compliance considerations.


